1. Workpiece Clamping in CNC Machining
The basic principles of positioning and clamping primarily involve the rational selection of locating datums and clamping schemes. The specific principles to be followed are:
(1) Strive for consistency among design, process planning, and programming in terms of datum reference;
(2) Minimize the number of clamping operations, and aim to machine all required surfaces in a single clamping and positioning setup.
2. Basic Principles for Selecting Fixtures in CNC Machining
(1) The coordinate orientation of the fixture relative to the machine tool should be fixed, and the dimensions of the workpiece and the machine tool coordinate system should be coordinated as much as possible.
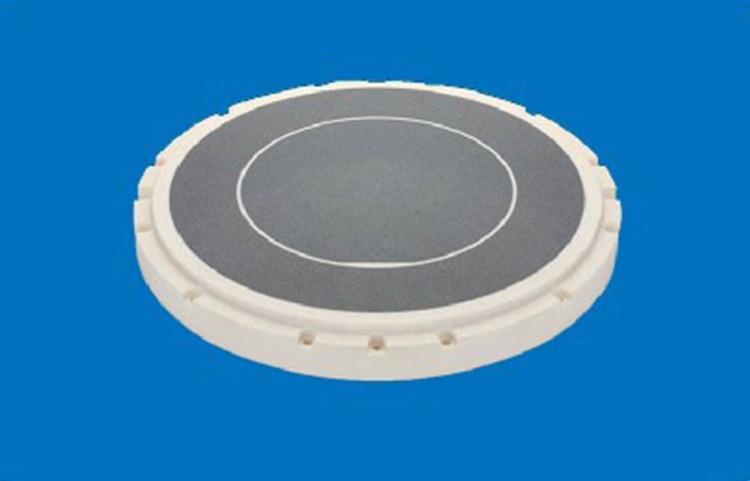
(2) If the production volume is not very large, modular fixtures, adjustable fixtures, or other versatile fixtures should be used as much as possible to shorten production time and reduce production costs.
(3) For batch production, dedicated fixtures may be considered, but the fixture structure should be as simple as possible.
(4) Loading and unloading of workpieces should be quick, convenient, and reliable, and the fixture components should not obstruct the machining of any surface of the workpiece.
3. Machining Errors in CNC Machining
Machining errors in CNC machining mainly include programming errors, machine tool errors, positioning errors, and tool setting errors.
Programming errors: These are errors generated during the programming process, consisting of approximation errors and rounding errors.
Machine tool errors: These mainly include errors in the CNC system and the feed system.
Positioning errors: These are errors generated during the positioning of the workpiece or fixture.
Tool setting errors: These refer to errors generated when determining the relative position between the tool and the workpiece.